The Gold Standard for Purity: Food Grade Magnetic Separators Built for Safety
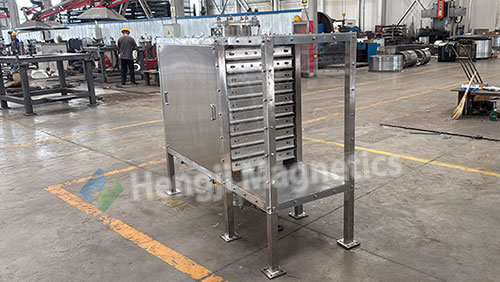
What separates an industrial magnet from a true food grade magnetic separator? The distinction starts at the very source of materials. For an inline magnetic separator to truly earn its certification, each component must adhere to uncompromising standards from selection through final verification. This commitment ensures absolute safety and regulatory compliance in your sensitive production environment.

Foundational Principle: Eliminate Risk, Ensure Compliance
The core philosophy is unambiguous: the equipment must safeguard product purity, never compromise it. Every element of our food grade magnetic separators—from direct-contact surfaces to structural frames—is chosen and validated against the highest benchmarks for food safety, hygienic design, and chemical resistance. This systematic approach transforms a simple inline magnetic separator into a validated component of your HACCP plan.
Critical Focus 1: Uncompromising Standards for Product-Contact Materials
This area represents the primary defensive barrier in any processing line. The materials that directly interact with your food or pharmaceutical product define the ultimate safety ceiling. We engineer our food grade magnetic separators with this non-negotiable priority in mind, eliminating contamination risk at its origin.

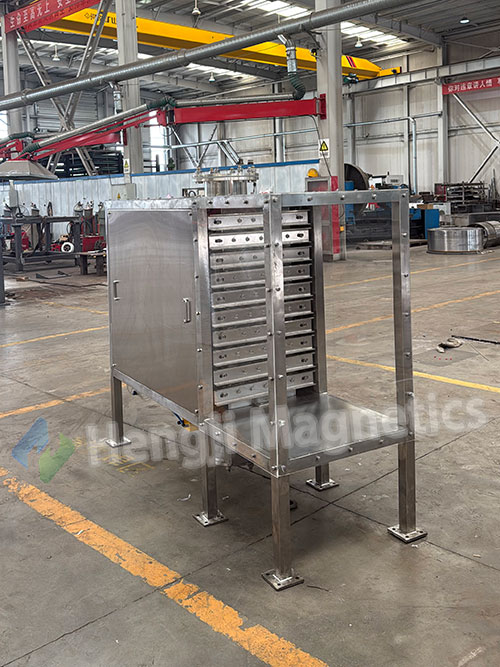
Stainless Steel: Certified Alloys with Superior Finish
All wetted surfaces in our inline magnetic separator utilize certified SUS 304 or 316/L stainless steel, backed by full material traceability. Beyond alloy specification, we achieve a critical sanitary surface finish. Contact areas are polished to Ra ≤ 0.8µm (with mirror finish available), creating a smooth, crevice-free surface that prevents microbial adhesion and enables thorough, validated cleaning protocols for your food grade magnetic separators.
Hermetic Magnetic Sealing: The Fail-Safe Barrier
The powerful neodymium magnets at our system's core are permanently isolated using a multi-stage sealing technology. Each magnet is individually protected before being hermetically encapsulated within a seamless, food-grade stainless steel tube. This engineered barrier in your inline magnetic separator undergoes rigorous pressure testing, guaranteeing lifelong integrity and eliminating any risk of magnetic material contacting your product stream.
Critical Focus 2: Rigorous Standards for Processing Zone Components
Even components not in direct contact must meet elevated standards. Parts exposed to the processing environment in our food grade magnetic separators are designed to prevent indirect contamination through dust, corrosion, or seal degradation.
Housings, Frames, and Hygienic Seals
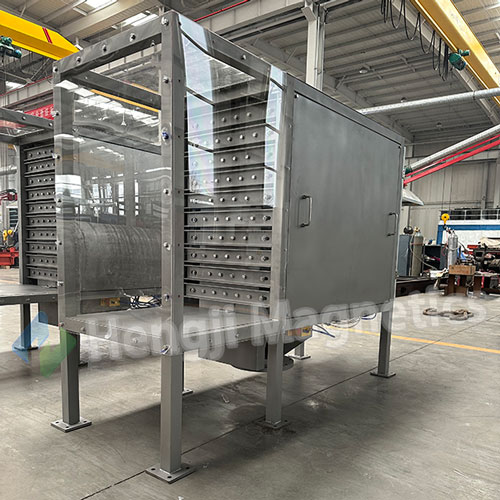
External structures are constructed from the same food-compliant stainless steels or FDA-recognized coated materials. Every seal and gasket in our inline magnetic separator is specified from FDA-listed, non-toxic elastomers like platinum-cure silicone, selected for exceptional resistance to high temperatures, steam, and aggressive cleaning chemicals. This preserves the long-term hygienic state of your food grade magnetic separators.
Critical Focus 3: The Verification Process: From Specification to Validation
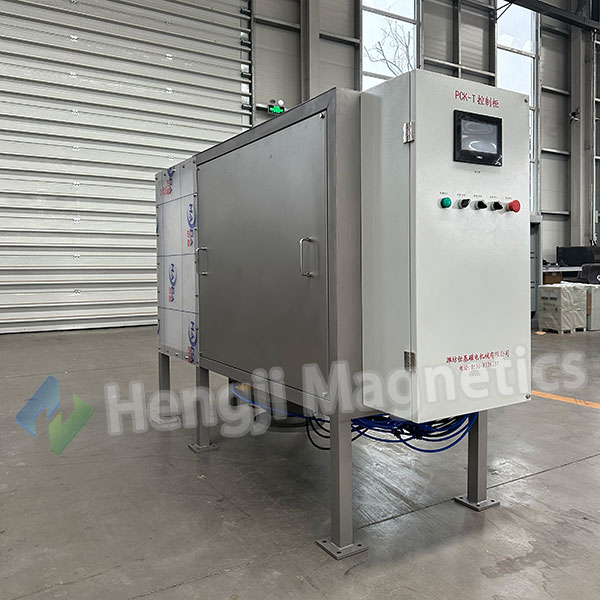
Establishing material standards requires an equally rigorous verification protocol. Our quality control system ensures every food grade magnetic separators unit meets its design specifications through documented checks and physical testing.
Stage 1: Documentation and Source Verification
We begin with comprehensive material certification review. Every component in your inline magnetic separator is supported by Mill Test Certificates for metals and compliance statements (aligning with FDA, EU, or NSF standards) for polymers and elastomers, ensuring full supply chain transparency.
Stage 2: Physical Testing and Performance Validation
We validate specifications with tangible evidence. Surface finishes are measured with precision instruments, and all critical welds—particularly magnetic tube seals—undergo visual and non-destructive inspection. Each magnetic assembly is subjected to stringent pressure decay testing, simulating years of operational stress to confirm the permanent seal in your food grade magnetic separators.
Stage 3: Controlled Final Assembly
Assembly of your inline magnetic separator is completed in a controlled environment. All components undergo a final cleaning process, followed by a white-cloth wipe test to verify the absence of manufacturing residues before shipment. This delivers a production-ready food grade magnetic separators unit.
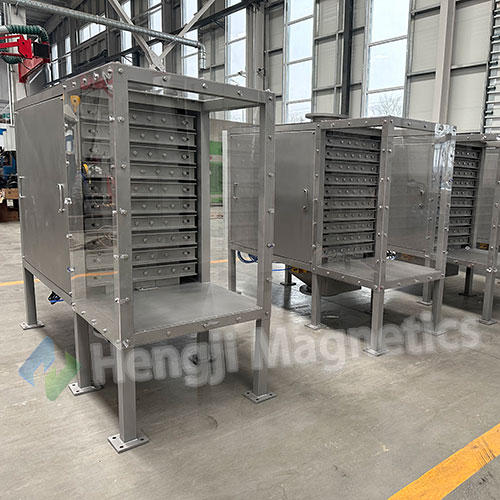
A Complete Safety Ecosystem
True food grade magnetic separators represent more than isolated components; they are part of an integrated safety ecosystem. This system combines certified material science with fail-safe mechanical design, supported by transparent quality assurance. The result is predictable, reliable protection for your most sensitive processes.
Your Guarantee of Compliance and Operational Confidence
This holistic engineering approach delivers more than equipment—it delivers certainty. Our inline magnetic separator solutions are designed to integrate seamlessly into your food safety management systems, acting as passive, dependable guardians of product integrity and brand reputation.
Invest in separation technology engineered with foundational integrity. Choose food grade magnetic separators built to meet the world's most stringent standards. Contact our specialists to configure the perfect, certified inline magnetic separator for your critical application.
Human-Centered Revolution: Simplifying Your Dry High Intensity Magnetic Separator
The Endurance Revolution: Say Goodbye to Replacement with Our Industrial Magnetic Separator
Related Article