
Resource Recovery and Waste Treatment
HENGJI MAGNETICS: Optimizing Mining Operations with Advanced Magnetic Separation
HENGJI MAGNETICS delivers cutting-edge magnetic separation solutions that revolutionize mineral processing efficiency. Our technologies boost productivity across three critical areas: pre-concentration waste rejection, wet processing grade enhancement, and tailings resource reclamation. Proven to increase recovery rates by up to 92%, reduce OPEX by 18-40%, and transform waste streams into profit centers – we empower mines to achieve new benchmarks in sustainability and ROI.
I. High-Efficiency Metal Recovery
Maximize value from complex waste streams
• Equipment:
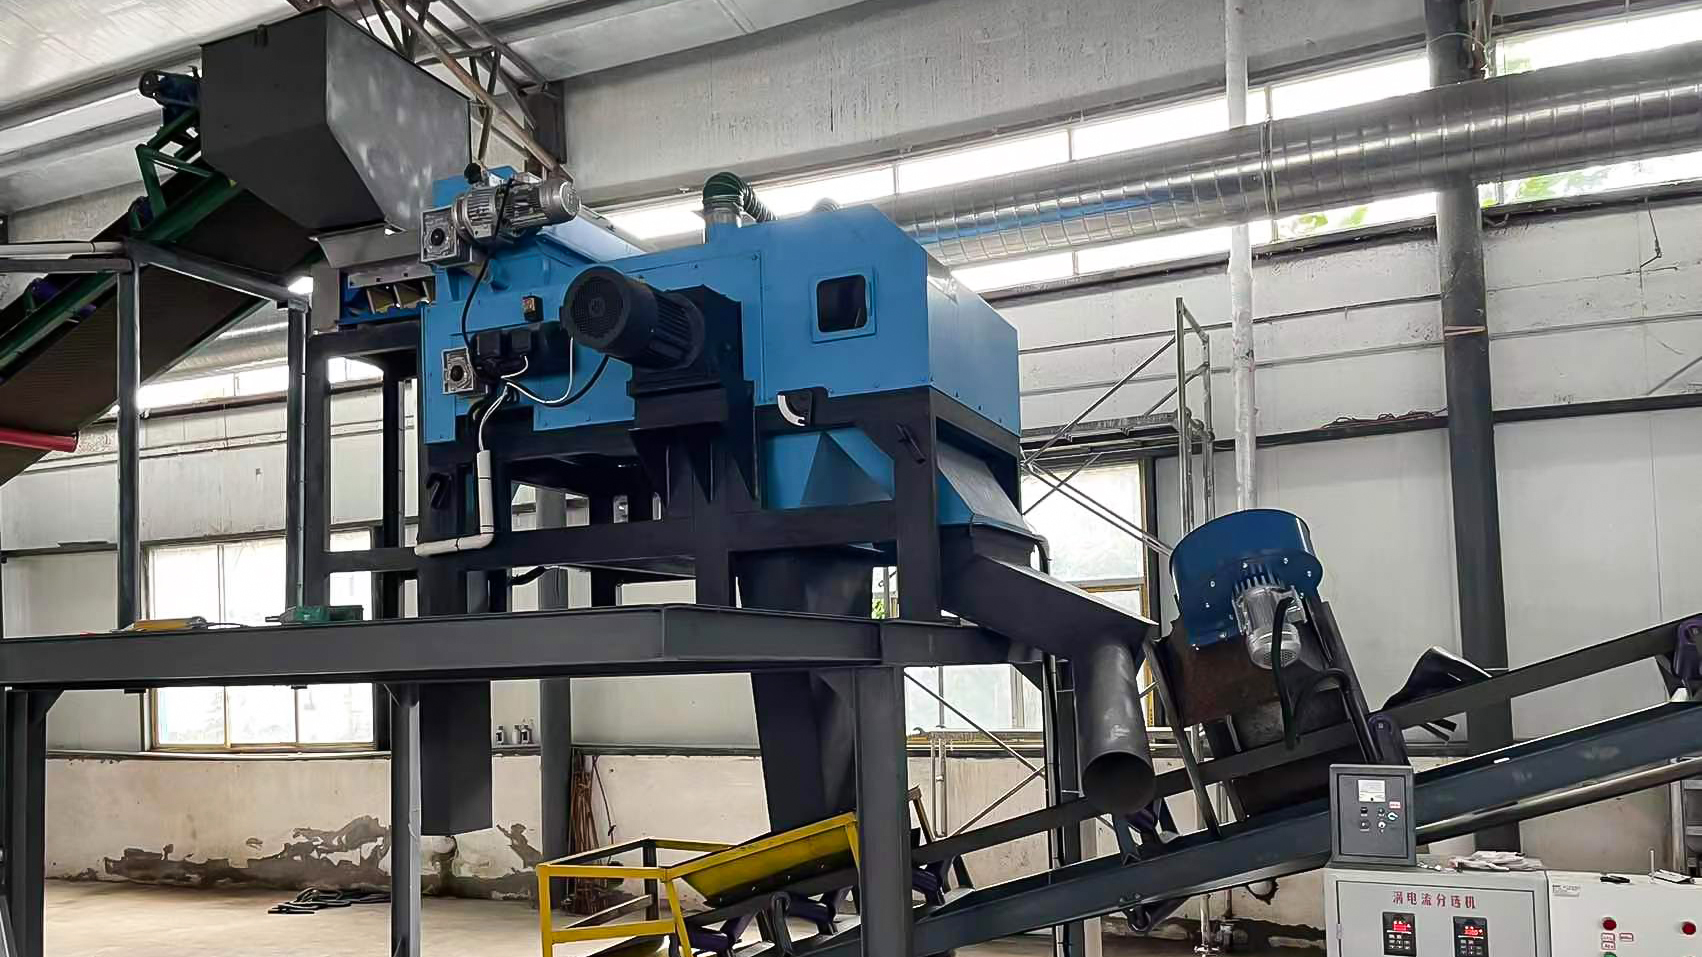
→ HECS Eddy Current Separators: Non-ferrous metals (Cu, Al, Zn)
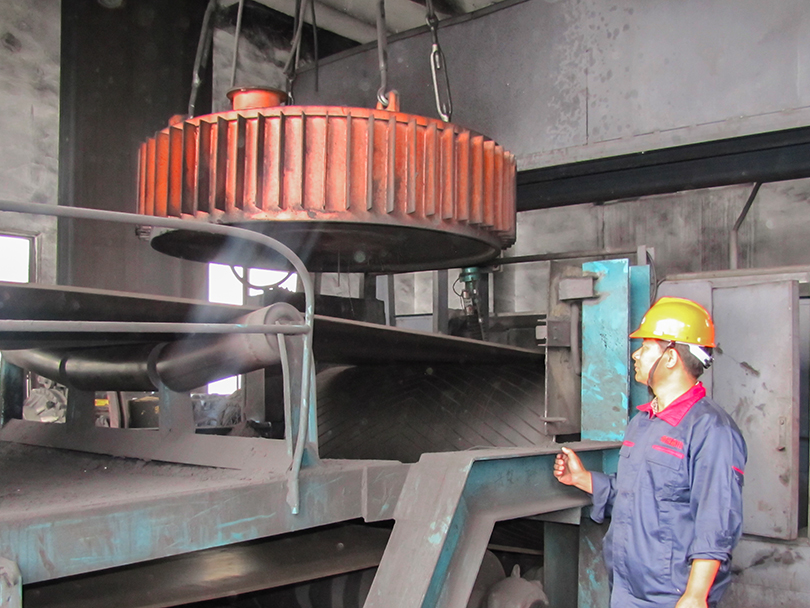
→ RCT Permanent Drums: Ferrous minerals (250°C heat-resistant)
Key Results:
✓ >99.5% Cu/Al purity | 98% recovery rate (vs. 80% industry avg.)
✓ 65% Fe concentrate grade | <1.5% residue loss (slag/red mud)
✓ 250°C operational stability (hot-stewed slag)

II. Hazardous Waste Detoxification
Achieve global compliance standards
• Equipment:
→ RCDB Electromagnetic Separators: Micron heavy metals (20,000 Gauss)
→ RCYF Inline Magnets: Fluid stream purification
• Key Results:
✓ >85% Cr/Ni retention (particles ≥5μm)
✓ 30% lower dioxin generation (EU BAT certified)
✓ 99.8% metal removal (fly ash/sludge)
III. Recycled Feedstock Purification
Enable food-grade circularity
•Equipment:
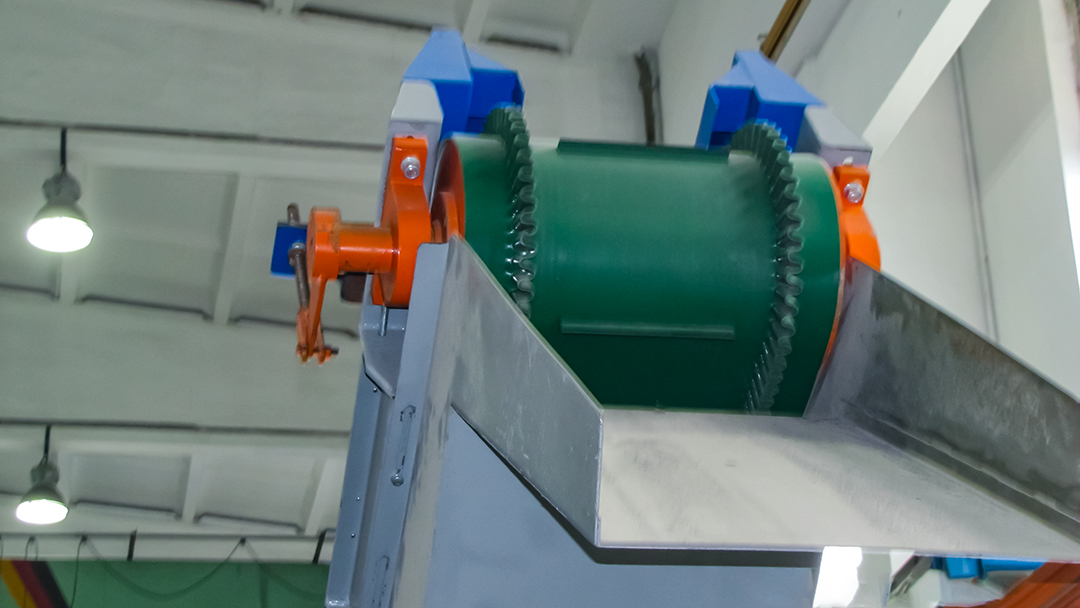
→ CTG Dry Drum Separators: Powder de-ironing
→ RCYA Pipeline Magnets: Gas/liquid flow interception
• Key Results:
✓ 99.8% metal removal (food-contact glass cullet)
✓ 50 t/h throughput | <0.01% Fe residue (plastic pellets)
✓ Full compliance with GB 13078/FSSC 22000 (feed/food safety)
Verified Success Stories
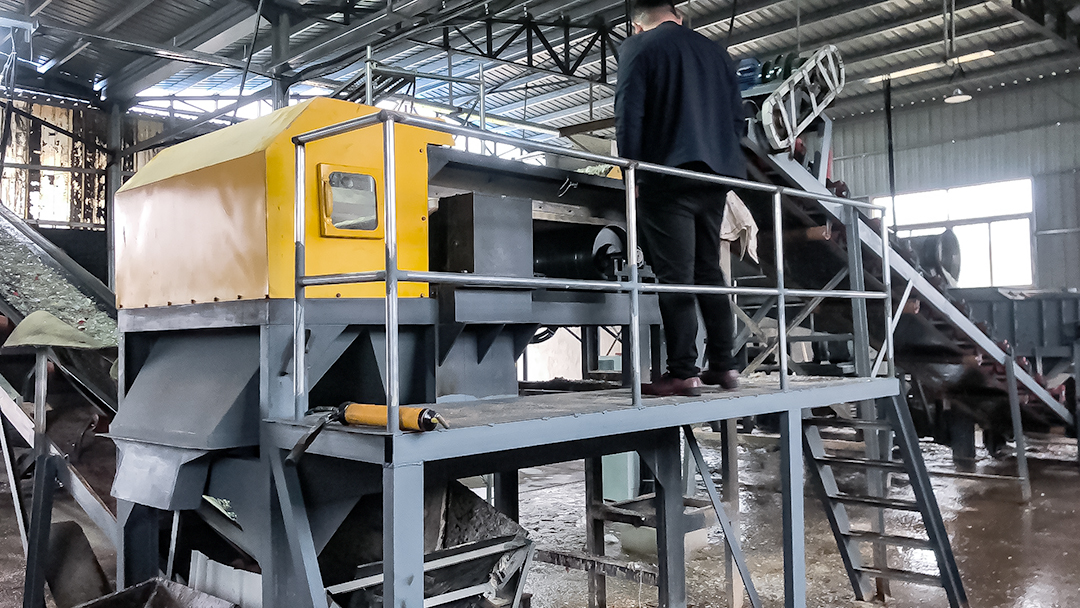
• E-Waste Metal Recovery: PCB Processing Line
▫ Client: Global recycler (Hubei, China)
▫ Solution: HECS Separator + RCYD Magnet
▫ Results:
→ 98% Cu recovery (99.5% purity) | 99.2% Al/Zn separation
→ $17.3M/year added revenue (30,000t waste PCBs)
→ *Audit Report: Doc-1*
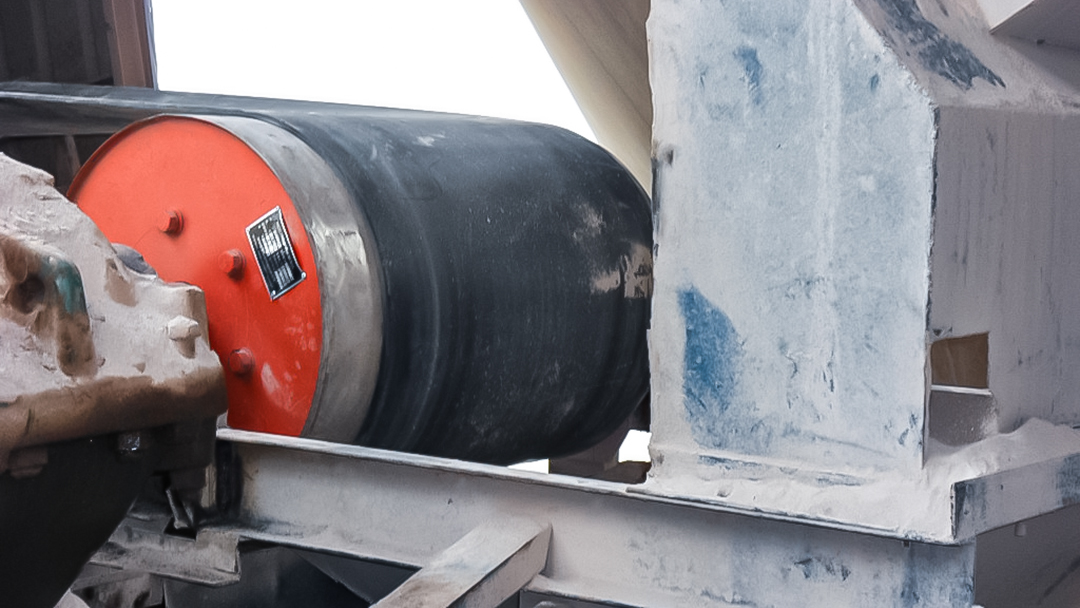
• Steel Slag Valorization: Hot-Stewed Residue
▫ Client: Leading steel manufacturer (Shanghai)
▫ Solution: RCT-250 High-Temp Drum
▫ Results:
→ 65% Fe concentrate | 0.8% residue loss
→ 220,000t/year recovered | $25.2M revenue
→ ROI payback: <30 days
→ *Validation: Doc-62*